Promoted
Rivers, Port-Harcourt, 2 hours ago
4 views
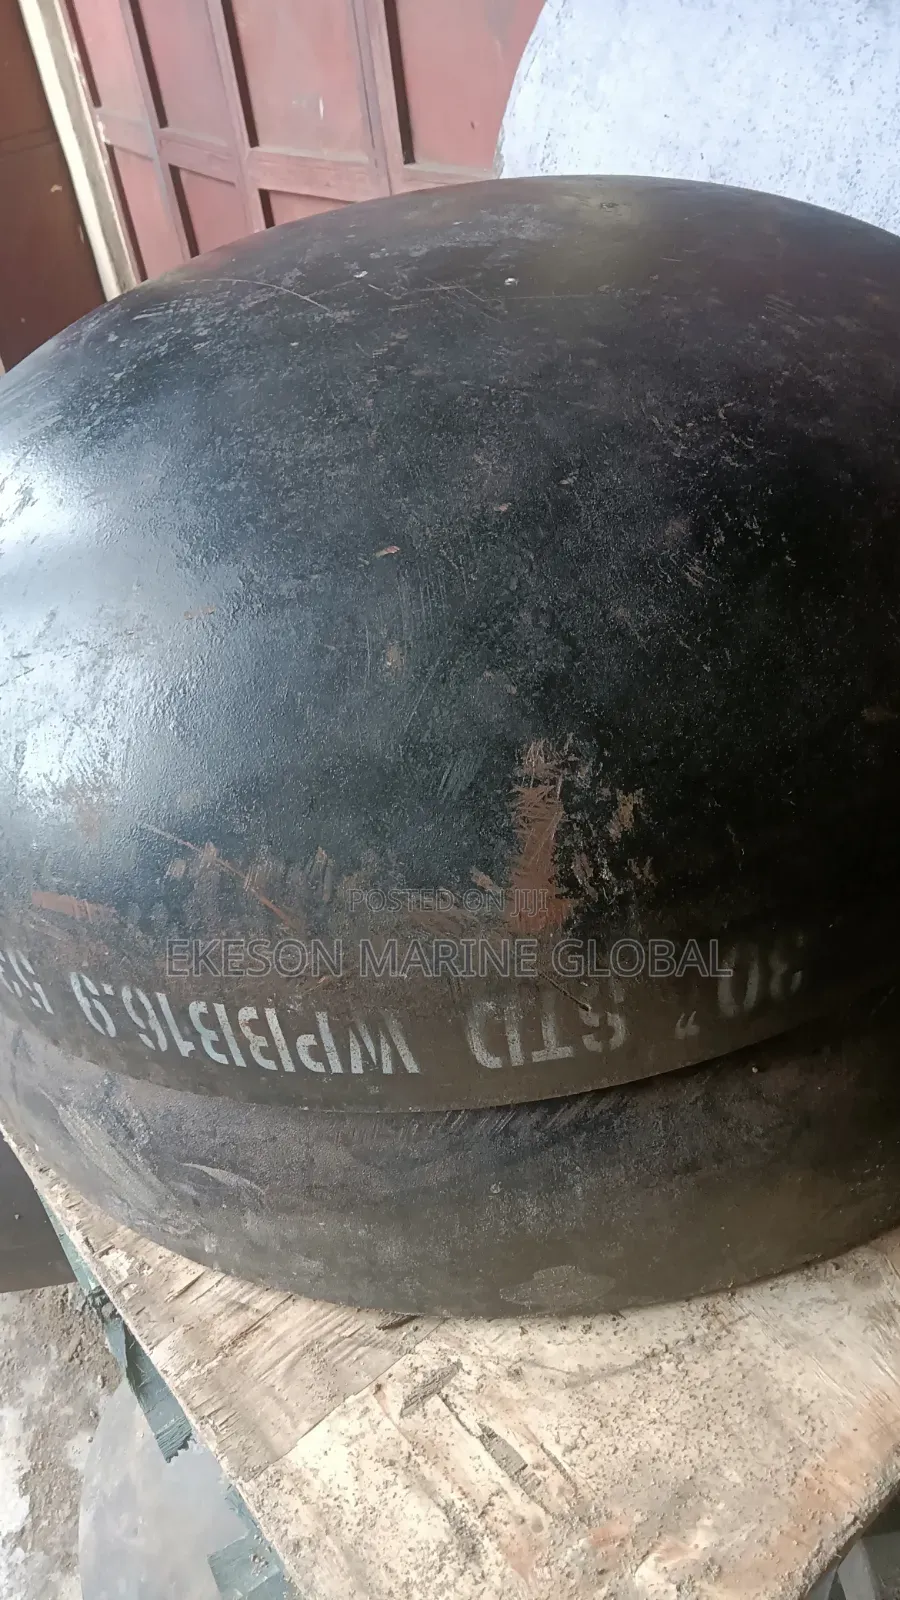
30" Welded Cap SCH 40 (All Sizes Are Available)
Brand New
Condition
Other
Type
Store address
Rivers State • Port-Harcourt
Mile3 building materials beside UST-ROUND ABOUT
Mile3 building materials beside UST-ROUND ABOUT
Closed now
• Mon - Sat, 06:58-12:00
When welding a 30" Schedule 40 pipe cap, you are working with a large-diameter, heavy-wall component (O.D. 30", wall thickness 0.375" to 0.500" depending on exact spec). Because of this size, it is most commonly welded using a Multi-Pass Butt Weld (GTAW + SMAW or FCAW).
Safety tips
- Avoid paying in advance, even for delivery
- Meet with the seller at a safe public place
- Inspect the item and ensure it's exactly what you want
- Make sure that the packed item is the one you've inspected
- Only pay if you're satisfied